Magnetic Drums
DEMZ® Sh Series Magnetic Drums
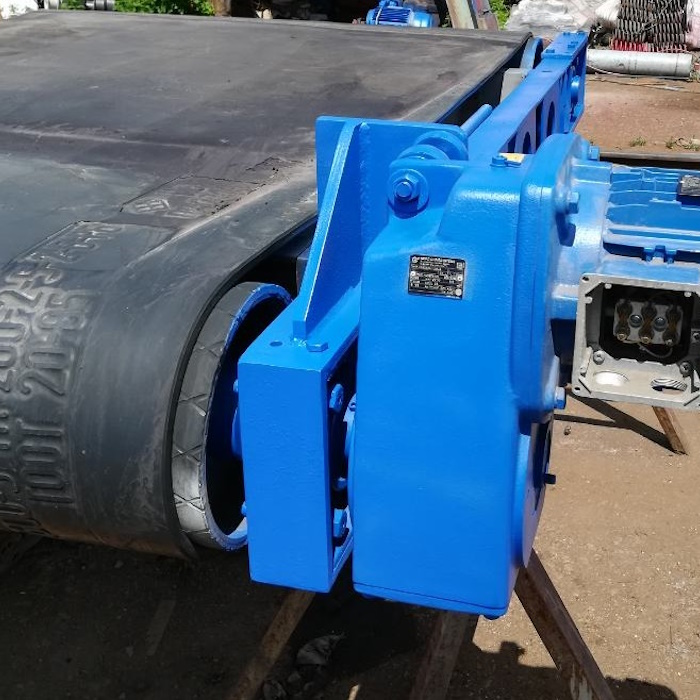
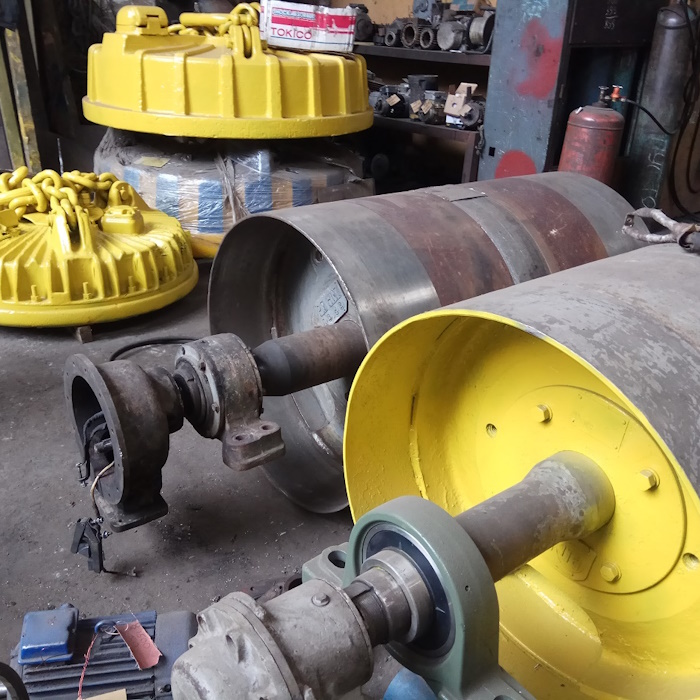
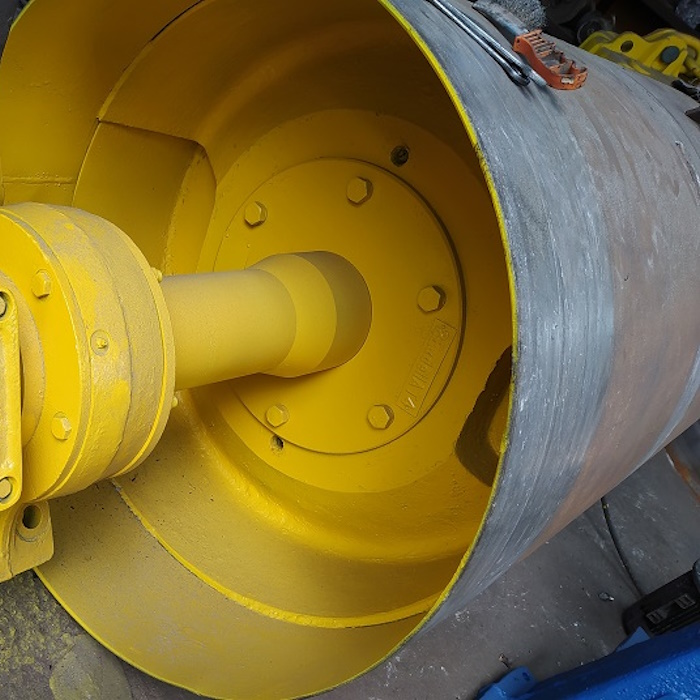
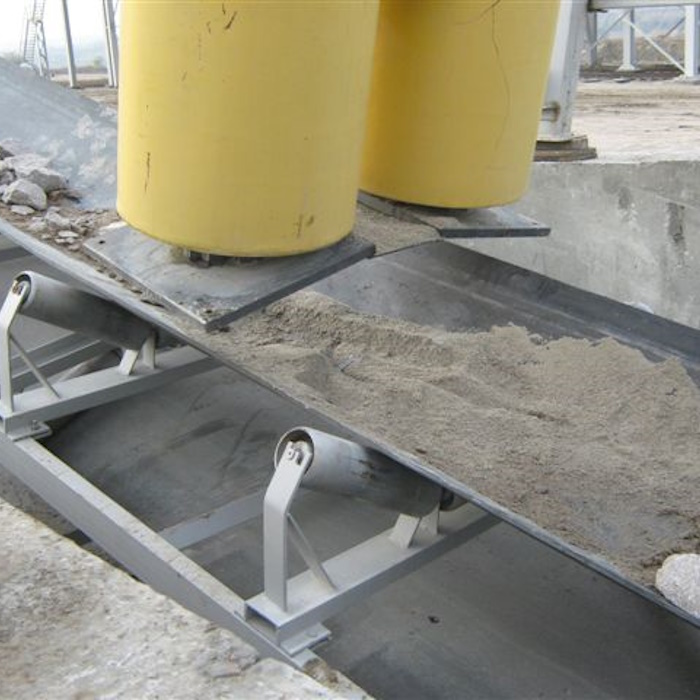
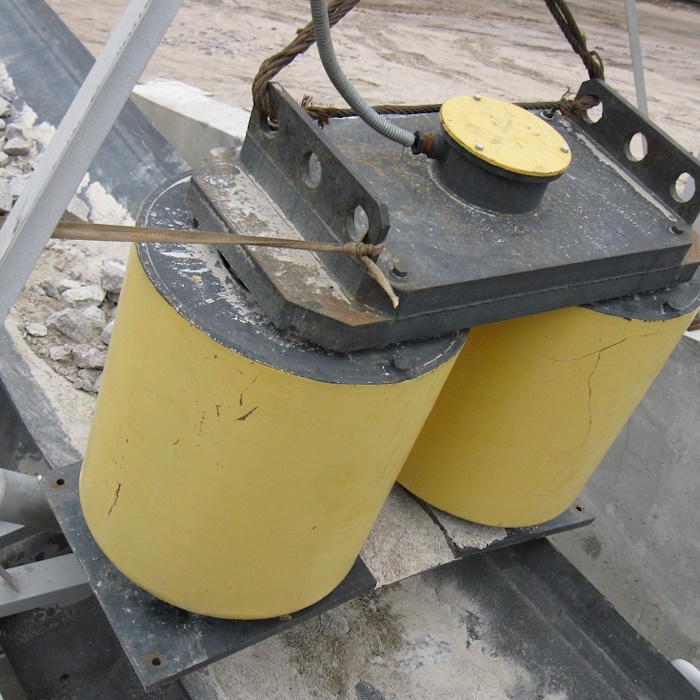
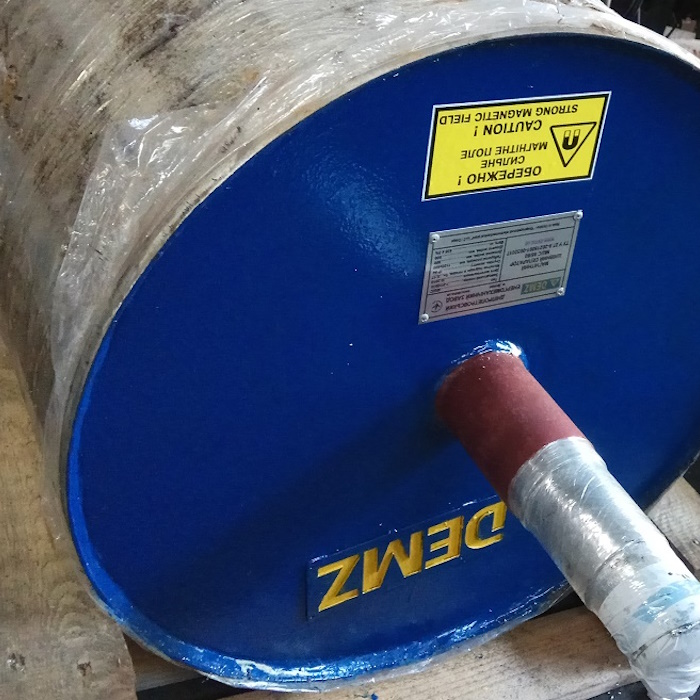
Magnetic drums are designed to extract ferromagnetic items from coal and other non-magnetic bulk materials transported by belt conveyors. They are manufactured in explosion-proof execution and can be operated in hazardous areas of coal preparation plants, screening facilities, coking plants, and other industrial enterprises. They are installed on belt conveyors in place of drive or non-drive drums. They are manufactured in direct current (DC) versions (ShE type) and permanent magnet versions (Sh type, magnetic system material: Nd-Fe-B, (BH) max > 320 kJ/m3). ShE-type electromagnetic drums are designed to remove ferromagnetic metal inclusions with an individual mass of 0.01–45 kg from a stream of various bulk and lump materials (molding sand, sand, etc.) moving on belt conveyors with a belt width of 500–1600 mm and a belt speed of up to 2 m/s. Electromagnetic drums are installed at discharge stations in place of drive or non-drive conveyor drums.
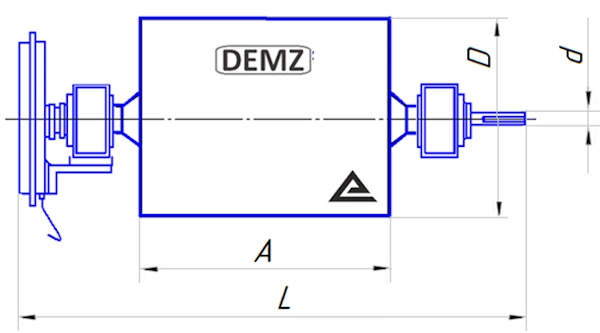
| ShE Type | Conveyor belt width, mm | Material layer thickness on belt, mm* | Rated power, kW | Dimensions, mm | Weight, kg | |
| L | D | |||||
| 5/5.3 | 500 | 150 | 1.0 | 1400 | 530 | 600 |
| 6.5/6.3 | 650 | 200 | 1.5 | 1500 | 630 | 800 |
| 8/6.5 | 800 | 200 | 2.0 | 1900 | 650 | 1000 |
| 10/8 | 1000 | 250 | 2.5 | 2100 | 800 | 2200 |
| 12/8 | 1200 | 270 | 3.0 | 2600 | 800 | 3000 |
* Depends on the magnetic properties, shape, dimensions, and movement speed of the extracted inclusion. Separator designs are subject to continuous improvement; therefore, technical parameters may differ from the values specified in the table.
Consultation
Our standards
Contact Us
Frequently Asked Questions (FAQ)
The lifting capacity of an electromagnet is the maximum load weight permitted to be lifted and moved by the magnet. It typically equals 0.5 of the breakaway (tear-off) force, providing a safety factor for secure operation.
The lifting capacity depends on the magnitude of the magnetic flux in the core. The flux increases as the magnetomotive force increases and as the magnetic reluctance of the circuit decreases.
Copper coils cost twice as much as aluminum ones; copper has 1.7 times higher conductivity than aluminum; copper density is 3.3 times higher than aluminum; copper’s specific heat capacity is 3 times lower than aluminum’s; copper coils offer more repair cycles and a longer service life than aluminum.
Welded steel housings are simple and cost-effective to produce. The advantages of a cast magnetic core over a welded one include cooling fins, greater operational durability, solid structural integrity, and the complete absence of internal air gaps.
Overheating, lower density of scrap metal, switching to metal stock with larger air gaps, and malfunctions in the control cabinet (voltage converter).
Improper operation (faulty control cabinet, overheating, moisture exposure, overvoltage), coil-to-housing breakdown (ground fault), open-circuit/broken conductors, and inter-turn short circuits within the coil.